
What Causes Progressive Layer Offset in Palletizing Robot Patterns? Coordinate, Fixture, and Product Inspection
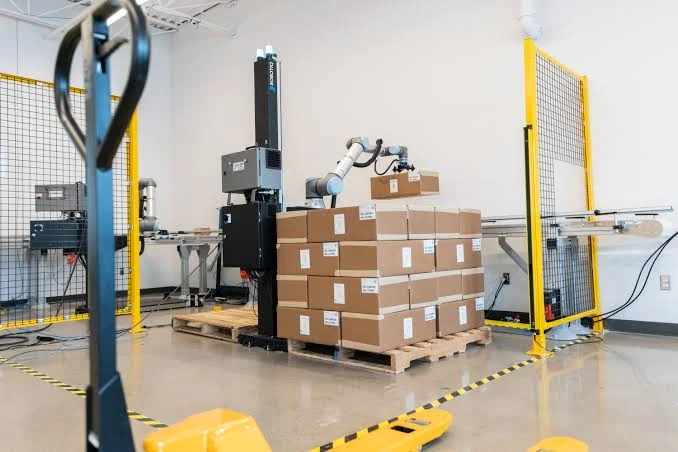
Progressive layer offset in palletizing positions may originate from workpiece coordinates, product dimensions, fixture center, gripping posture, conveyor positioning, and cumulative errors in the palletizing program.
In this article
When a palletizing robot's bottom layer position is normal but gradually shifts as the number of layers increases, one should determine whether the deviation is a cumulative error in a fixed direction, random variation, or only occurs at a specific gripping position.
- Key Inspection Points
- Measure the actual dimensions of the product, any deformation, and the repeatability of its positioning upon delivery.
- Check if the fixture's suction cups, grippers, positioning blocks, and Tool Center Point (TCP) are loose or worn.
- Verify the pallet position, workpiece coordinates, layer height, row/column spacing, and rotation rules.
- Observe whether the deviation is related to the robot's posture, load, or approach direction.
- Troubleshooting Steps
- Reproduce the issue using standard products and a fixed pallet to eliminate random errors from incoming materials.
- Recalibrate the fixture TCP, pallet workpiece coordinates, and conveyor positioning points.
- Check if the palletizing calculation is repeatedly accumulating uncorrected dimensional errors with each layer.
- Perform verification tests: no-load, single-layer, multi-layer, and complete pallet pattern.
- Common Misconceptions
- Manually adjusting program points for each layer without identifying the root cause of cumulative dimensional or coordinate errors.
- Only checking robot accuracy while ignoring variations in pallet and conveyor positioning.
- Continuing to use the original TCP after fixture maintenance.
- Summary
Progressive layer offset in palletizing positions may originate from workpiece coordinates, product dimensions, fixture center, gripping posture, conveyor positioning, and cumulative errors in the palletizing program.
Industrial Robot Repair Hotline: +86 18122009539
Contact Repair Engineer: +86 18122009539
Need a part or repair assessment?
Share the robot model, part number, fault details and destination country with our team.
Contact our team ↗